Showing posts with label Casting and Molding. Show all posts

Saturday, March 9, 2013

Trash Bashing a Sci -Fi Vehicle From Start to Finish: Part 2.

Trash Bashing a Sci -Fi Vehicle From Start to Finish: Part 2.


Now it just comes down to gluing and puttying everything into a nice solid mass. You can see here that I also used various thicknesses of styrene sheet to add panels, a door in the back, and other details. Now is when the real fun of trash bashing starts. Try to get a good overall amount of detail without leaving one area too sparse while overloading another. Although sci-fi vehicle design is often more whimsical than functional try to think about what your vehicle needs and what certain parts can represent. 

The Bates Industries Roadpig DX.
I use primarily cyanoacrylate glue but occasional epoxy glue when required. Milliput yellow-grey is used to fill gaps and sculpt details, like the seal around the cockpit bubble, that I can’t find good bits for. Milliput seems to work better for this than any other modeling putty since it sticks pretty well and can be smoothed with water before sanding once it’s cured. I’ve found that wetting the area that I’m going to apply it to helps it to stick better while trying to blend joins and transitions. 

The rear door, leading to storage and the engine compartment, is scratchbuilt out of styrene. The taillights are plastic hemispheres that I found in the craft section. They usually come with an adhesive on the back but I scraped this off to make sure that super glue would stick. They are based on circles of styrene punched out using a bunch of various sized punches that I’ve collected.

Try to add several layers of detail to heighten visual interest.
For the wheels I used soda caps with their edges sanded smooth and then glued in pairs. The axel housing is just a hunk of balsa wood covered in sheet styrene. I carved out an indentation in the top to allow the rounded container to fit snugly on it. I use balsa wood to build forms like this since it’s quicker than trying to build a whole shape out of styrene and it’s much stronger as well.


A twelve-pack of Diet Mountain Dew gave its life so that this car could roll.
The hubcaps are made using Insta-Mold from Cool Mini or Not. This is a very useful low-temp melting silicone that allows you to make simple castings. I made a master part using a washer and some of the craft hemispheres. These were then cast using various putties. This gives a more regular feel to the piece and is much easier than trying to scratchbuild each part.


This stuff is great for making multiple copies of that one really neat greebly that you only have one of.
All of the parts are glued on and puttied I usually go over it again with medium grit sandpaper before painting. Then I go over it lightly with a damp paper towel to get rid of the worst of the sanding dust. 

Next up Priming and Painting!

Molding and Casting


Molding and Casting...For Beginners
By Jay "Cozmo" Curtiss - images & text © 2003 The following is what I consider to be the most painless way to cast replicas of a part that I want to have several of, but don't want to build each individually. I am a firm believer in the KISS method. So this may seam over simplified to some of y'all. Though most mold making kits come with instructions, I have yet to see one that was easy to understand. I will try to do better. Since most of us don't have vacuum chambers and pressure pots, we won't worry about that stuff.
I started casting my own parts about 15 years ago, with latex one-piece molds and polyester resin, gun turrets and fittings for 1/96 scale ships mainly. Not long after I began, I did some contract work for a model shop. While there I learned the basics of making molds with RTV (Room Temperature Vulcanizing) silicone. I wish I had studied it more. At the time I thought you had to have lots of equipment and capital to make those kinds of molds. This is by no means the only way to make molds. Or even the best way for you; it works for me.
Recommended Supplies
  • Mold compound, comes in many different varieties. If you get the kind that gets mixed in weight ratios you need an electronic scale. For this exercise I will use a 1:1 volume ratio mold compound. You can get this at several places. And you can get it, and casting resin, in trial sizes as well. I got mine from Smooth-on. I have heard that Micro-Mark now handles this as their 1:1 ratio mold compound.
  • Legos, to build the mold box.
  • Liquid latex, to seal the mold box. You can get this at most well stocked hobby or craft stores.
  • Stir sticks, craft sticks, toothpicks and skewers. To mix the compounds and chase air bubbles, for both the mold compound and resin.
  • [Click to enlarge]

    ^ Recommended supplies
  • Disposable brushes, for applying the latex and mold compound.
  • Disposable measuring and mixing cups.
  • Rice, to measure the volume of mold compound needed.
  • Double-sided carpet tape, to secure the part to be molded and the mold box.
  • Modeling clay, (the non-sulfur kids kind). This is mainly for two part molds. You set the part to be molded in clay up to the widest part of the object. Pour the mold compound, let dry, remove the clay without removing the part, apply a mold release (so the mold compound does not adhere to itself), and pour the second part.
  • Talcum powder (release agent), to dust the inside of the mold so the part will come out easier. You need a bonified release agent when making two part molds to keep the RTV silicone from sticking to itself.
  • Some pieces of acrylic, just a little larger than the projected size of the mold.
  • Some weights, just heavy enough to hold the acrylic sheet steady on the mold. Before You Mold: The Master
    The object that you want to mold is known as the prototype, or master. Every detail of the master will be reproduced by the mold. So, this is the best time to get rid if those scratches, gouges and sanding marks. RTV silicone and latex molds can handle small undercuts. Undercut is used to describe an area of a cast part that is larger than the opening of the mold, so the mold has to be stretched to get the cast part out. If there are many, complex, or large undercuts it is better to make the mold in more than one piece.
    Decide how you want to cast the part. Flat parts are easy. Others, like cylinders, are more difficult to decide. You can either set it on end (and have one end with no detail) or cut the part in half lengthwise, make a mold of both halves, then assemble the cast pieces. However you decide, a little forethought can make the entire process go a lot easier.
  • [Click to enlarge]
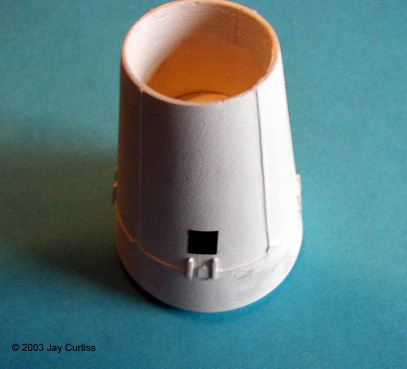
    ^ Master and mold box [Click to enlarge]
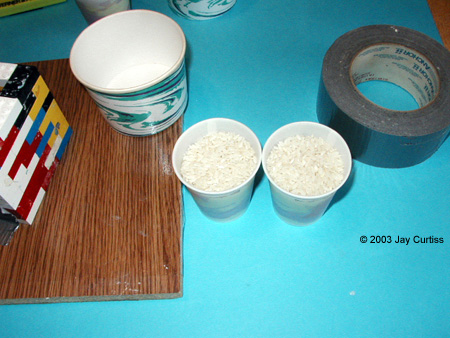
    ^ Using rice to determine the amount of mold compound required [Click to enlarge]
    ^ Ready to pour the mold []
    ^ Piece of acrylic and weight on a one piece mold [Click to enlarge]
    ^ The cured mold appears as the mold box is disassembled [Click to enlarge]
    ^ Some one-piece molds
    Two-part Molds
    [Click to enlarge]
    ^ Mold box, part and air channel for 2nd part of mold ready to pour [Click to enlarge]
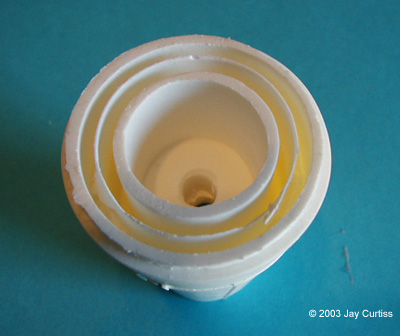
    ^ Two piece molds disassembled and ready to have the cast parts removed, note the resin sprues lower left and bottom of the CM. The mold for the CM is the only one that is assembled, and held together with a rubber band, before filling with resin. There is a fill hole and a hole for trapped air to escape. The mold is tilted so the air hole is at the highest point of the mold. [Click to enlarge]
    ^ The reward: all of the casting is done, now to build the model [Click to enlarge]
    ^ Some two-piece molds. Arrows mark where locating "pins" have been formed to aid aligning the separate mold pieces.
    Step One: Preparing the Mold
    Begin by building a box around the part to be molded. Lego's come in real handy for this. Don't skimp on the size in this step. You want there to be enough of the mold to hold its shape. A half-inch ought to do.
    Place the part to be molded into the box, fill with rice to the desired height of the mold. Pour the rice equally into two measuring cups and mark the cups. This is how much of each part of the compound we will need.
    Seal the mold box with latex and let dry. On a clean level surface (I use a scrap of shelf board) place enough double-sided tape to secure the entire mold box. Put the part to be molded firmly onto the tape. Since this will eventually be a two-part mold I also put some locating pins. Locating pins help to properly assemble the mold. Then place the mold box around the object and press firmly into the tape.
    Step Two: Pouring the Mold
    During this process it is important to do everything possible to avoid air bubbles.
    Mix the mold compound according to the manufacturer's directions. Use a lot of newspaper, as this part can be messy. In addition to whatever the instructions tell you, do everything you can to avoid air bubbles while mixing. They can ruin a mold.
    Use a disposable paintbrush and "paint" the object to be molded with the compound. This way you will be sure to fill any undercuts or areas that can trap air bubbles.
    Place the mold box at a slight incline and pour the mixture slowly into the lowest part of the box. Always looking for trapped air and piercing any bubbles you might see with a toothpick.
    After the recommended curing time you can carefully remove the mold box, remove the master part and you are ready to cast new parts.
    If there are any air bubbles, mix a small portion of mold compound and fill in the bubbles with it. You can also repair a torn mold this way.
    Casting
    In choosing a casting resin I like to get a low viscosity (less than 80, flows almost like water and fills most all areas) medium cure (pot life about 7 minutes and can be removed from the mold in about an hour) resin. The resin cures by generating its own heat through chemical reaction. The smaller the part cast, the longer it takes to cure. It is usually not a good idea to mix less than an ounce of resin at a time. It's hard to get a good enough mixture to cure.
    Have some pieces of thick acrylic, weights, talcum powder, mold release (you can use the stuff for candle making or "Pam" type cooking spray) and some toothpicks. A couple extra molds and some small round containers. These are to hold any extra resin, good for carving or turning new parts.
    Give the mold a good dusting of the talc, and spray the acrylic with a mold release.
    Measure and mix the resin according to the manufacturer's instructions.Again, during this process it is important to do everything possible to avoid air bubbles.
    Pour the resin into the mold to fill. If there is trapped air, use a toothpick or skewer to remove them. Pay attention to the time so you are not still removing bubbles when the resin starts to harden.
    Place a piece of acrylic over the mold. Do not put it straight down, but rather start on one side and lay it across the mold. This pushes air bubbles over the side of the mold instead of into it. You can then place a weight on the acrylic to remove extra resin from between the mold and the piece of acrylic. Just make sure that the weight is not so much that it deforms the mold.
    When the resin has cured, you can remove the acrylic from the mold. Extra resin will have formed a thin "wafer" that will hold small parts together. This can either be cut, or sanded away.
    If you are spending an afternoon of casting, you can do the pouring on one of those large magazines that comes with the Sunday newspaper. That way you can just tear out the page after each pour and remove all the overflow. You can start the next pour with a clean surface.
    And there ya' go. A copy of the original part in much less time than it would take to make one from scratch. Now you can make as many as want.
    Two-Part Molds
    Here is where things can get tricky. Rather than start all over with a new subject, I will show how the one-piece mold I just made will become a two-piece mold. Before I begin to make the second part of the mold, I will cast one of the parts so the copy, rather than the original, will be modified for the molding process.
    Most two part molds are used to replicate more detailed parts with many under-cuts. They must be secured together and have fill holes and holes for air to escape. The second part of this mold will be to hollow out the part to save weight and form the "garage" for the kit supplied Lunar Module (LM). Instead of assembling the mold first, the resin will be poured first, and then, the mold assembled.
    Once the part to be molded has been modified, it is placed back into the mold in the exact position it was removed. The first part of the mold already has locating pins formed into it. If it didn't they would have to be carved into the mold.
    A mold release agent is then applied to the mold and part to make sure the new part of the mold can be separated from the old part. Just to be on the safe side, liquid latex is also applied here the RTV silicone will touch. A mold box is also built around the mold up to the height that the second part of the mold will reach. This too is covered with latex.
    When the mold is assembled, there is the possibility that the process will trap air in the mold. To keep this from happening, a channel is made in the new mold by inserting a plastic rod vertically into the center of the new mold where it meets the old one. The new mold will be formed around this rod. Make sure the air channel does not get larger as it travels through the mold. Resin will fill this chamber as the mold is assembled, and the cured resin, that filled the channel, will need to be pulled through the mold to remove it. Build something onto the mold box to hold the rod steady. To show that anybody can screw up, I had planned for this channel to be an accurate escape rocket, but I put the lower half in upside down when making the first part of the mold. The locating pins were to double as the engine bells for the escape rocket.
    Like with the one-piece mold, use the rice to determine the amount of mixture, then mix and pour the mold mixture according to the instructions. Let the mold cure.
    Carefully disassemble the mold and you are ready to go.
    Casting the Two-Part Mold
    You cast the two-part mold the same as the one-part mold. After you pour the resin, place the second part of the mold into the first part, matching the locating pins. Depending on the size of the second part of the mold, the resin does not have to completely fill the mold. While filling, tip and roll the mold slightly to get the resin to coat the interior of the entire mold (this helps eliminate air bubbles). The second part of the mold will push the resin up to fill the mold.
    Where to Get Stuff

    Rhino Chassis part

    Space Marine Rhino Chassis part 3

    Welcome back everyone for the final part in the 3 part Rhino scratch built tutorial.  When this is finished you will be able to see how we plan to make this a completely modular vehicle which can be easily changed to weapon load outs that represent Razorbacks and Predators (which will be for future tutorials).  This is where we left off in Tutorial 2-


    Materials:
    Tank bits:  Tank wheels (3/4", 19.050mm) OR posterboard, tank tread (3/8" wide, 9.525mm) OR plasticard, top hatches
    Stick pins
    1/16" (1.588mm) x 1/32" (.74mm) Neodymium Magnets
    Plasticard (For Sale signs)
    2 part Resin (optional)

    Tools:
    Pin Vice
    1/16" drill bit
    Hobby Knife
    Sand paper
    InstaMold (optional)

    Next we will work on the wheels for our Rhino.  For the more detailed wheels, take a GW Rhino wheel rim piece and carefully trim the top until it can sit in the wheel well with about 5/16" (7.938mm) exposed.  Take your InstaMold and form around the detailed half of the wheel rim.  Duplicate the wheel rim 20 times, keeping in mind you only need each rim to be 3/16" (4.762) wide (the width of the open wheel well).


    Taking the two halves, glue them back to back so the straight top parts are even.  Do this for the other 9 sets and begin by placing one directly in the center of the wheel well on either side.  At the front angle and back angle, place yet another set of wheels.  Evenly space the rest as it appears in the image below.


    If you aren't using the resin/InstaMold, you can make your wheels with 3/4" (19.05mm) circles cut from the posterboard.  Cut 20 out, split into pairs, and as above trim the tops to allow for about 5/16" (7.938mm) to be exposed at the bottom of the tank.  Place these as suggested above.

    Now that the wheels have been placed, it's time to add our side doors.  If you haven't cut out the doors found in the template here, do so now.  Sand the edges down slightly to remove the hobby knife bumps and place on the side of the tank directly centered between the two exhaust pieces.  Using your pin vice, drill two holes 3/8" (9.525mm) from the top and sides just enough to make a dent into the side of the tank.  Place your magnets into the side of the tank and the doors.


    Next, cut out the top door hatches from the same template if you haven't already.  Again, sand the edges down a little to remove where the hobby knife caused the plastic to raise.  Measure 1/2" (12.7mm) each of the straight sides to determine where to drill with the pin vice.  Do the same with the other hatch.


    Place the doors on the top of the tank and line up the edge 5/8" (15.875mm)  from the rear of the tank.  Using the holes you already created, drill slightly into the tank through each of the 4 holes.  Add your magnets in the same fashion as you did for the side doors.


    Taking your tank tread bit, remove the bumps from the bottom section and make a mold of the tank tread using your InstaMold.  Pour the 2 part resin into the mold and allow it to cure.

    Rubber mold I had already made previously

    After it cures but is still a little soft, remove the tank tread and begin by dabbing glue on the center wheel and the two wheels that go to the back.  Trim any excess quickly and starting in the center drape the piece across the tank wheels, carefully curving the back half up to the top of the wheel.  Cut the excess tank tread to allow for the rest to be tucked nicely into the opening just above the front wheel.


    After the tank tread cures fully, repeat this process with the remaining 3 sections where the tank treads go.  After these all cure, you may remove any side flash from the tank treads with a hobby knife.  Alternatively, you may cut a long strip of plasticard which is 3/8" (9.525mm) wide.  Score (not cut through) along the strip every 1/4" (6.35mm) on one side and place onto the wheels so the scored side is showing.  Bend the plasticard so that it forms around the front wheel up into the wheel well all the way back to the rear wheel.

    With your pin vice, Drill holes in all the places where there are rivets showing in the images below.  After completing this, cut the stick pins so there is just the head and a little bit of pin left.  Safely discard the other half or keep somewhere safe to use for pinning other models.  Glue the pins into the holes and your rivets will be completed.


    Either duplicate the top hatches using InstaMold and resin or find these bits from another source (as they are super hard to duplicate and look good doing so).  Add these to the top of the tank so they line up with the front view ports.


    For a finishing touch, take a stick pin and place it at the rear corner of the tank to represent an antenna.  Remove the side doors and place a hole direction between the magnets on the tank's side using your pin vice.  At the top, do the same directly between the 2 sets of magnets.  This won't make much sense now, but in future tutorials it will allow for adding side sponsons and weapon load outs above to convert into Predators and Razorbacks.

    Well, that finishes up the SB40k Rhino tutorial.  As always, if something doesn't seem to be adding up or seems off, leave a comment below and I'll do my best to explain or fix the error (which does happen, of course).  Good luck with your scratch building and for the next conversion I'll be looking at adding some interesting bits to our little tank!

    Press Molding small bitz

    Press Molding small bitz

    So I won a large lot of Necromunda Orlocks on eBay awhile back.  Three of the four heavy weapons models had no weapons or backpacks.  This makes me a sad panda.  So here is a quick tutorial on how to re-create the missing way oop parts. 

    You will need one original to create the copy from!


    You will need a flat clean work area, I am using a piece of plastic card here
    I recommend Legos to build the mold box
    Next place Instant Mold in hot (not quite boiling) water until it is soft and pliable. Place the instamold in the bottom of the box and press your bitz around halfway into the IM.  Allow the IM to harden at room temperature or place in the fridge. 
    First half of mold is filled.
    Next heat up another portion of IM and cover the other side of the Bitz, then cool as before.
    Second half of mold is filled.


    Once cooled to room temp remove the mold from the box and slowly separate the IM halves.  Mix up your green stuff or ProCreate putty and pack both halves of your mold.  Re-align your mold halves and press them together slowly squishing the excess greenstuff or Procreate out, you will probably need to trim some of the excess off before it sets. I use very strong clamps and small boards of MDF when pressing the mold halves together.


    I use Procreate at a 60-40 mix per the instructions for a hard curing sand able finish.


    Mold half with ProCreat bitz in it

    Original compared to the copy
    Above is a photo of the original and re-cast bitz,  Mold making time is around 30 minutes. The ProCreate sets up in around 4 hours, I let these set up while I was at work and I cleaned the mold lines after I got back home.  ProCreate continues to harden over the next 48 hours or so, meaning mold lines are easier to clean sooner than later.
    Best part of this is I can reuse the Instant Mold for the next project or lost bit.

    More examples:
    All of these came from eBay, missing weapons.  The weapons are press mold copies made of ProCreate and the front 3 have copied backpacks.

    These vents are press molded from Green Stuff.

    Sculpting Tools and Putty

    Sculpting Tools and Putty

    SCULPTING PUTTY

    Epoxy putty is a two-part substance that hardens by chemical reaction once the two parts are combined. Commonly, miniature gaming figures are sculpted from a plumbing putty that will withstand the heat and pressure required for the mold making process. This putty comes in a blue part and yellow part that combines to a bright green color. Original sculptures, regardless of the color of the putty used to create them, are still commonly referred to in the industry as "greens".


    What kept me from sculpting miniatures for many years was the inability to control the material of the actual "green stuff". I had compared it to sculpting with bubblegum. When I first tried my hand at it in the mid 90s there was no internet resource or community accessible for an isolated noob. After jumping back into the hobby again in late 2005, I discovered there was a wealth of info online and promptly completed my first few sculpts. I still didn't like green stuff very much because it was so different from the plastilene and polymer clays I was already so familiar with.

    So, taking lots of tips from pros and others in the hobby I began to experiment with different putty mixing trying to get a better workability to what I was used to. The most frequently asked question I get is about the difference between green stuff and brown stuff. I have summarized it to this:

    Green Stuff is a two part epoxy putty that has an elastic property making it suitable for organic sculpting. It stays quite flexible after curing. This also makes carving, drilling, sanding or scraping extremely difficult.

    Brown Stuff is an epoxy putty the has a more traditional clay-like feel to it making it suitable for non-organic sculpting, like weapons and armor. This makes it very suitable for carving, drilling, sanding or scraping. This also makes it brittle and very susceptible to breaking.

    Initially, I mixed the brown and green putties to get the best properties of both and greatly reduced the frustration of their downsides.


    Then, in July '06 ProCreate was marketed and I found a superior all-in-one putty that works for everything. Depending on the mix of white to black the cure and hardness will be affected. I personally prefer mixing it at a 1:1 ratio. It can be carved, drilled, sanded or scraped with good results.
    In all respects ProCreate works and behaves pretty much like the green/brown putties. The biggest advantages to me are the lack of "memory" (elasticity which makes fine details extremely difficult to get sharp), low tack (works well with an assortment of tools) and the overall neutral color (no green screaming into my eyes). There are a couple of things to watch for, though. When mixing it, there is a noticeable residue left on your fingers. This will create a "slip" if water is used as a lubricant during mixing. Be sure to wash your hands after your sculpting sessions. I cannot stress how unsanitary it is to lick your sculpting tools, that is defintely NOT recommended when working with this particular putty. Also, it seems to be very gooey when fresh from the package. I store my putty in little plastic jars and dig out a certain amount to work with. If this sits exposed for a couple of days, the hardener will firm up a little and make the putty more workable (unless you like it gooey).

    ProCreate and other putty is available through these fine online suppliers:
    Kraftmark - manufacturer's site
    Heresy Miniatures
    Jeff Valent Studios
    The War Store


    It is also worth mentioning another couple of putties that are extremely useful which are Aves Apoxie sculpt and Magic Sculp. Both of these are formulated differently from the green or brown Kneadatite and even the ProCreate.


    According to the Aves web site, Apoxie® Sculpt offers economy as well as performance. This 2-part product has a putty-like, smooth consistency, and is easy to mix & use. It is safe and waterproof with 0% shrinkage/cracking! Working time is 2-3 hrs. Cures hard in 24 hrs., and has a semi-gloss finish. Adheres to plastic, resin kits, wood, metal, ceramic, glass, polymers, foam, fiberglass, & more! Can be seamlessly feathered before set-up, or sanded, tapped, drilled, carved, lathed, or otherwise tooled after set-up, without chipping, cracking or flaking.

    Magic Sculp's web site says it is the two-part epoxy putty specifically designed to meet the needs of modelers, crafters and sculptors alike. One of the only epoxies that will smooth out with water. Its grain structure is finer than any other product available and will not shrink or crack even when formed in large structures. It can be shaped by hand or with modeling tools, sanded, carved, painted; you can attack it with a grinding tool and the cured material will not break apart or lose its shape. Magic Sculp will cure at room temperature.

    Both of these putties have similar properties to Milliput Superfine White, but are less expensive than importing Milliput from England.

    Curing is something the putty does on its own through a chemical reaction. Since the material is not polymer clay (like Sculpey, Fimo or Cernit) it does not need to be baked at higher temperatures for it to harden. You may hear sculptors refer to a "putty oven" and "cooking" their sculpts. This is similar to an Easy Bake Oven for your putty. Higher temperatures cause the putty to cure at a faster rate. Most putties have a working time from 1 to 4 hours and up to 24 hours for a solid cure. Sculpting in stages allows greater control over details and permits working on specific areas of a sculpt at a time. Rather than waiting four hours for a weapon to cure before it can be attached to hand, you can "cook" the putty under a hot lamp and then after it cools for a few minutes, proceed with completing that portion of the sculpt.


    My cooker is a custom built job from a one gallon sized paint can, aluminum work light, a 60W bulb and some bit of cork. I trimmed the lamp shade with old scissors and epoxied the light to the top of the can. A similar rig can be made with a large coffee can.

    Molds for the sculpts during the vulcanization process can run between 300F and 330F. I have clocked the temp of my putty oven at just over 200F which is plenty enough to make sure it is thoroughly cured before going to mold. I like to leave my sculpts in there from 20 to 45 minutes depending on thickness.

    The opposite is also true, the cure time of putty can be slowed by placing it in the freezer. If you have mixed putty you'd like to use at a later time (like after lunch or an episode of TrueBlood) you can place it in the freezer to slow the curing rate. I don't have any data on how long it actually extends the working time but I've left it for a couple of hours and it was still workable. I also store my packages of extra putty in the freezer until I get ready to use it.

    TOOLS
    Here is how I have now pared down my essential tool collection. The tools I use the most are the absolutely necessary #64NW Double Ended Dental Pick which is similar to the Wax #5 tool. It is my "go-to" tool for about 80% of all my sculpting tasks. I had to grind a sharper edge on it and then keep it smooth with nail polishing pads. My other favorite tools are the Spoon Shaped Putty Knife # 60738 , a flat chisel and round tapered color shaper, a disposable #11 scalpel which has been dulled a bit with sandpaper or a file, and a "pokey" tool which has a couple of different sized needles on each end.
    Other useful items are a container for water. I use a spent plastic blister pack with a bit of foam in it to make a sponge. This is handy to keep your tools wet without saturating them. I stick some blobs of putty onto a plastic divider from those Plano plastic case inserts. This makes it easier to cut off bits of putty to mix without having to dig it out of the packages each time. You can also use a plastic swatch cut from a clean milk jug instead of the dividers. I cover this with a bit of plastic wrap when not being used to keep it free of particles. A quick rip peels the plastic right off.
    I also have a little spritz bottle of rubbing alcohol handy to keep my tools clean. Uncured putty cleans right up with a bit of rubbing alcohol. Vaseline petroleum jelly is very handy for lubricating tools and various smoothing techniques. If you experience trouble getting fresh putty to stick on areas that are cured after using Vaseline to smooth them, clean the area with a bit of rubbing alcohol first before applying the fresh putty. Alcohol can also clean metal to remove the talc powder that is used in molds and the putty will stick better. Purell handy wipes work wonders at getting your hands and tools clean too.

    THE PROCESS
    Although in these examples I am using Pro-Create putty, it was a process I developed using regular green and brown stuff. So it is suitable for those putties as well.
    Normally I will wet my cutting tool and slice off a chunk of the white part. Then I clean the blade so as not to contaminate the black part, wet the tool again and then cut a chunk of that the same size of the first. Cutting the putty this way allows me to get an exact amount to mix and produces less waste.

    I knead the two parts folding them over and over until the color is uniform. I tend to over-mix my putty a bit after the color is smooth. This firms it up a little and assures both parts are blended.
    Swatches of plastic are very handy for creating all manner of items. Here I use the divider from a Plano plastic case insert again. I find these little dividers very durable and will not curl up under the heat of a putty oven like milk carton plastic tends to do.

    Here I begin by sticking the putty to the plastic card and begin to shape a pile of stones for a figure's base.


    Once the putty has cured, I use my cutting tool to carefully pry the part, in this case a pile of stones, off the plastic divider. This technique is very useful for creating swords, shields, guns, bases and other objects. Two-sided items like guns can be made easily by sculpting one side first and then after completing all the details and curing, the item is popped off and the opposite side is detailed.

    Plastic wrap is also very useful! It is extremely handy in smoothing large areas, especially with a bit of Vaseline applied. Once the area has cured, the Vaseline can be cleaned off with a little alcohol and fresh putty applied for the next stage. The best trick I learned from a class with Werner was belts and straps. A blob of putty can be stuck to plastic wrap and then cut to shape. By popping the shape off of the plastic wrap with the side of your scalpel, it can be applied to the sculpture and then smoothed into place. The best plastic to use for this technique is heavy freezer storage bags cut into 2" squares.

    This rambling collection of tips hopefully has encouraged you to give sculpting a go. It wasn't intended to give any instruction in actual sculpting, that is a whole 'nother topic! But, this should give you a good starting point to using and handling various sculpting materials. If you are already doing figure conversions, you are half way there to making full figures. Give it a shot!